Last Updated: October 23, 2026
Quick Summary
To automate recurring industrial supplies, gather three months of purchase history per item, calculate reorder points from average usage and lead time, then set automated replenishment rules with min/max levels. Start with one consumable category, draft orders for human approval first, and add approval limits before turning on automatic release.
- Gather at least three months of purchase history per item, pulling invoice lines rather than order totals.
- Calculate reorder point as average daily usage times lead time in days, plus safety stock.
- Set safety stock at roughly half the usage swing for steady items and the full swing for critical items.
- Build recurring purchase orders on a cycle set from usage data, and include a skip option.
- Run the first month with every automated order drafted for human approval before enabling automatic release.
Table of Contents
- What You’ll Need Before You Automate
- Step 1: Map Your Usage and Set Industrial Supply Reorder Points
- Step 2: Build Automated Inventory Replenishment Rules
- Step 3: Set Up Recurring Purchase Orders
- Step 4: Choose Manufacturing Procurement Software
- Step 5: Add Approval Controls, Budgets, and PO Policies
- Common Mistakes to Avoid When You Automate Recurring Industrial Supplies
- How to Measure Whether Automation Is Working
- Frequently Asked Questions
What You’ll Need Before You Automate
Automating how to automate recurring industrial supplies starts with two things: clean usage data and a purchasing setup that can actually handle repeat orders. Most shops jump straight to software and stall out. The ones that succeed do the boring prep first.
This guide comes from the team at IBEX Enterprises, where we supply sanding and grinding abrasives, tools and protective gear to woodworking, metal fabrication and autobody shops.
Here’s what most guides get wrong: they treat automation as a software purchase. It’s really a data and approvals project that happens to use software.
Pick one consumable category, such as sanding discs in your two most-used grits, and automate just that first. A single working category teaches you the rules, lead times and approval flow before you scale.
The Data to Gather First
You need three months of purchase history per item, at minimum. Pull invoice lines, not just order totals.
- Item descriptions and manufacturer part numbers
- Quantity bought per order and how often
- Unit of measure, so you don’t mix boxes with sleeves
The Accounts and Approvals to Set Up
Before any system fires an order, decide who can approve what. Set spending limits per person, per department and per order value. Name a backup approver for holidays and vacation. Confirm your accounting team’s requirements for purchase orders, because retrofitting that later is painful.
Step 1: Map Your Usage and Set Industrial Supply Reorder Points
A reorder point is the stock level that triggers a new order. Get it right and you stop both stockouts and dead stock.
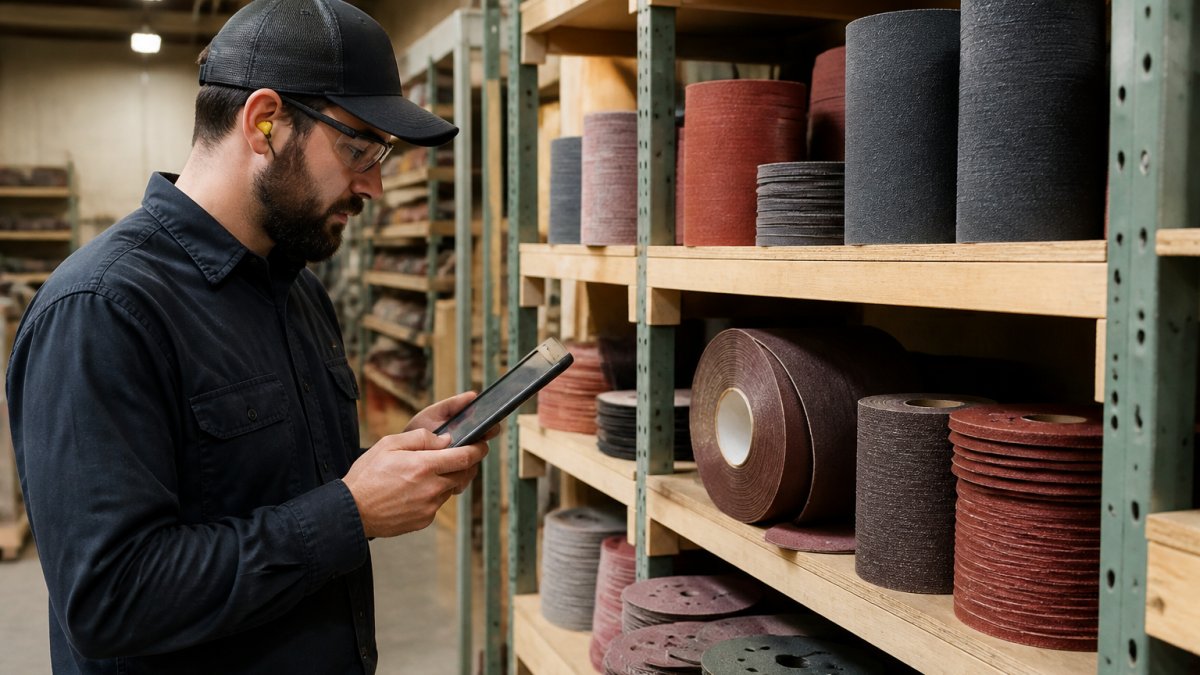
Start by calculating average daily or weekly usage for each item. Then look at how much that usage swings.
Walk the shelves with a tablet and count what’s actually there. Physical counts beat system counts almost every time in small shops, because returns and breakage never get logged.
How to Calculate a Reorder Point
Use this formula: reorder point = (average daily usage × lead time in days) + safety stock.
Say a shop uses 6 sanding discs a day and the supplier delivers in 5 days. That’s 30 discs to cover the lead time. Add a safety stock of 10 discs for a busy week. The reorder point is 40 discs.
Recalculate quarterly, or any time your product mix changes.
Setting Safety Stock When Usage Swings
A single average hides the weeks that hurt you. Pull twelve weeks of usage and note the highest week and the lowest week. If the high week is more than about 50% above the average, your safety stock needs to cover that gap, not the average.
A practical method most shops can run without a spreadsheet model:
- List weekly usage for the last 12 weeks per item.
- Subtract the lowest week from the highest week. That range is your usage swing.
- Set safety stock at roughly half the swing for steady items, and the full swing for critical items you cannot run out of.
- Add the safety stock to the lead-time demand from the formula above.
Example: a shop uses between 18 and 46 sanding discs a week, averaging 30. The swing is 28 discs. For a critical grit, set safety stock at 28 discs.
Adjusting for Lead-Time Variability
Lead time is rarely fixed. If your main supplier normally delivers in 5 days but has stretched to 12 twice this year, build the reorder point on the longer figure for critical items.
Track actual delivery dates against order dates for your top suppliers. After three months you will see which suppliers are reliable and which need a longer planning horizon.
Set reorder points separately for your top two or three grits and grades rather than one blanket rule per category. Usage on a 120-grit disc is rarely the same as on a 36-grit, and a shared rule will either overstock one or starve the other.
A Simple Min/Max Worksheet
Before you touch software, build a one-page worksheet per item with these columns:
- Item and manufacturer part number
- Unit of measure (box, sleeve, each)
- Average weekly usage
That worksheet becomes the input to your replenishment rules in the next step. Shops that skip it usually end up rebuilding their rules from scratch within a quarter.
Step 2: Build Automated Inventory Replenishment Rules
Automated inventory replenishment means the system places or drafts an order when stock hits a set level, without anyone checking a shelf. The rules you set here decide whether that works or creates chaos.
Set three numbers per item: reorder point, minimum level and maximum level. Then decide whether the system drafts a purchase requisition or places the order outright. For most shops, drafting first and letting a person approve is the safer start.
Min/Max Levels and Stockout Safeguards
Min/max levels cap how much you hold. The minimum is your reorder point plus a cushion. The maximum is what fits your shelf space and budget without going stale.
Stockout safeguards worth building in:
- A hard flag on critical items, so they can never be skipped
- An alert when a supplier’s lead time slips past its usual window
- A review trigger when usage jumps well above the rolling average
Step 3: Set Up Recurring Purchase Orders
Recurring purchase orders are scheduled orders that repeat on a set cycle, such as every second Tuesday or the first of each month.
Set the cycle from your usage data, not from habit. If you burn through a case of discs every 10 days, a monthly cycle leaves you short.
Build in a skip option. Shops that can’t pause a recurring order end up stockpiling supplies they don’t need during slow periods.
Step 4: Choose Manufacturing Procurement Software
Manufacturing procurement software handles catalogs, approvals, purchase orders and receiving in one place. The right choice depends on how your suppliers send product data and how your accounting team wants orders to arrive.
This is the section most guides skip, and it is where automation projects actually succeed or stall. The software is the easy part. The hard part is connecting it to the way your suppliers and your books already work.
Judge any option on four things:
- Does it hold your supplier catalogs with real part numbers?
- Can it handle punchout to supplier sites?
- Does it support EDI for larger suppliers?
How Supplier Catalogs Actually Work
A hosted catalog is a file of your supplier’s products, part numbers, units of measure and prices that the procurement system loads and keeps current.
Hosted catalogs are cleaner for repeat items because the part numbers and units are fixed. Punchout is better for suppliers who change pricing or stock often, or who carry a wide range you only occasionally buy.
Ask each of your top suppliers three questions before you commit:
- Do you provide a hosted catalog file, and how often is it updated?
- Do you support punchout, and which procurement platforms have you connected to before?
- Can you accept purchase orders by EDI, and what document types do you support?
EDI and Accounting Integration in Plain Terms
EDI, or electronic data interchange, moves orders, acknowledgements and invoices between systems without retyping. A supplier that supports EDI can receive a purchase order the moment your system sends it, confirm it automatically, and send the invoice back the same way.
Not every supplier supports EDI, and small abrasive or tool suppliers often do not. That is fine. The point is to know which of your suppliers can, and to route those through EDI while the rest take emailed purchase orders from the same system.
On the accounting side, confirm two things: that the system can export or sync purchase orders and receiving records into your accounting platform, and that it can match invoices to purchase orders so your bookkeeper is not reconciling by hand. Ask your accountant which format they prefer before you choose a platform, not after.
Skipping the integration check is the most common reason automation projects stall. Confirm your top three suppliers can accept orders the way the software sends them before you sign anything.
A Practical Rollout Sequence
Do not switch every supplier and every item at once. A sequence that works for most small shops:
- Load catalogs and part numbers for your top consumable category only.
- Connect the accounting export and test one purchase order end to end.
- Run the first month with every automated order drafted for human approval.
- Once the drafts are consistently correct, turn on automatic release for the steadiest items.
- Add the next supplier or category only after the first one runs clean for a full cycle.
This staged approach costs a little more time up front and saves far more than it costs, because problems surface while they are still small.
Step 5: Add Approval Controls, Budgets, and PO Policies
Controls are what stop automation from becoming a spending leak. Set them before the first automated order goes out.
- Spending limits per person and per department
- A second approver above a set order value
- Monthly budget caps by category
Review the automated order log monthly for the first quarter. You’ll usually find one or two rules set too loose.
Automation without approval limits just makes it faster to overspend. Set the controls first, then turn on the ordering.
Common Mistakes to Avoid When You Automate Recurring Industrial Supplies
The biggest mistake is automating every item at once. Start with your steadiest, highest-use consumables, prove the rules work, then expand.
Other traps we see:
- Using system counts without a physical check. Bad counts produce bad orders.
- Ignoring lead time changes. A supplier who slips from 5 days to 12 will cause a stockout if your reorder point never moves.
- Setting min/max levels from a single busy month. Build rules on typical usage, not your best week.
How to Measure Whether Automation Is Working
Track a small set of numbers monthly. If they don’t move, the rules need work.
| Measure | What it tells you | Target direction |
|---|---|---|
| Stockouts on critical items | Whether safeguards work | Down to zero |
| Ordering admin time per week | Time saved on reordering | Down |
| Emergency or rush orders | Whether reorder points are too low | Down |
| Inventory value on hand | Whether max levels are too high | Steady or down |
| Order accuracy | Whether catalogs and part numbers are clean | Up |
Review these against your pre-automation baseline. A shop that cuts emergency orders and keeps steady stock is winning, even if the savings are hard to pin to one line item.
Frequently Asked Questions
How do you set reorder points for industrial supplies?
Multiply your average daily usage by your supplier lead time in days, then add a safety stock buffer for demand swings or shipping delays. A shop using 20 sanding discs a day with a 7-day lead time and 3 days of safety stock sets its reorder point at 200 discs. Review the figure quarterly, and raise it before busy seasons or when a supplier’s lead times stretch.
How can a business automate recurring supply orders?
Start by choosing a supplier that supports scheduled shipments and purchase order payments. Load your recurring items into their ordering system, set quantities and delivery frequency, and connect your approval workflow so each scheduled order routes to the right person. From then on, orders generate on schedule without manual entry, and you only intervene when usage changes or a budget threshold is hit.
How do you prevent overstock when automating recurring orders?
Cap order quantities at a maximum level based on storage space and shelf life, and schedule a monthly review of slow-moving SKUs. Abrasives and consumables do not expire quickly, but tying up cash in excess stock still hurts. Set the recurring order to pause automatically when stock on hand plus open orders exceeds the max level, and adjust frequency rather than quantity when usage drops.
What information should an automated reorder system track?
At minimum: current stock on hand, open purchase orders, average daily usage, supplier lead time, reorder point, and maximum stock level for each SKU. Add unit cost and budget code so approvals route correctly, plus a last-ordered date to flag items that have gone dormant. That combination lets the system trigger replenishment at the right moment and gives you an audit trail when someone asks why an order went out.
Getting recurring industrial supplies right is mostly about discipline: clean data, sensible reorder points and controls that keep spending honest. IBEX Enterprises builds that into the ordering itself, with automated recurring shipment subscriptions, purchase order payment support and rapid reordering from a personalized dashboard. If you want your abrasives, tools and protective gear to arrive on a schedule instead of a scramble, request a quote and we’ll set up a plan around your usage.