Last Updated: October 26, 2026
Quick Summary
To manage abrasive inventory, build a stock control spreadsheet that tracks on-hand quantities, usage rates, and reorder points, then calculate reorder points as average weekly usage times lead time plus safety stock. Store abrasives dry and in original packaging, rotate stock FIFO, and track turnover and stockout rate monthly.
- Reorder point equals average weekly usage times lead time in weeks, plus safety stock.
- Set safety stock at one week of usage for steady demand, two for seasonal, three for custom or long lead time.
- Keep coated abrasives in original packaging, stored flat and dry, away from docks and compressors.
- Start barcode labels on the top 20 percent of SKUs that drive most usage, then expand.
- A shop consuming $48,000 CAD with $12,000 CAD average inventory turns stock 4 times per year.
Table of Contents
- Why Abrasive Inventory Control Decides Whether Your Shop Keeps Running
- Step 1: Build Your Abrasive Stock Control Spreadsheet Template
- Step 2: Run an Abrasive Reorder Point Calculation That Holds Up
- Step 3: Apply Industrial Abrasive Storage Best Practices
- Step 4: Choose Abrasive Inventory Tracking Tools That Match Your Shop
- Step 5: Rotate Stock with FIFO and Lot Traceability
- Step 6: Standardize SKUs and Track the KPIs That Matter
- Common Mistakes That Undermine Abrasive Stock Control
- Frequently Asked Questions
Why Abrasive Inventory Control Decides Whether Your Shop Keeps Running
Abrasive inventory is the stock of coated abrasives, belts, discs, wheels, and blasting media a shop keeps on hand to keep sanding and grinding work moving. At IBEX Enterprises, we see the same pattern across shops: the sander stops, the job sits, and someone drives across town for a box of discs. A stockout on a critical grit costs more than the abrasives themselves.
The Real Cost of a Stockout on the Line
Picture a cabinet shop mid-batch. The 120-grit belts run out on a Friday afternoon. The finisher waits, the spray schedule slips, and the customer hears about it. That is the real cost of poor stock control: idle hands and broken promises.
Most shops carry too much of the wrong grit and too little of the right one. Fixing that starts with a simple system, not a bigger shelf.
What You Need Before You Start
Gather these basics before you build any tracking system:
- A list of every abrasive you use, by grit and size
- Rough usage counts from the last three months
- Supplier lead times for each item
Step 1: Build Your Abrasive Stock Control Spreadsheet Template
An abrasive stock control spreadsheet template is a simple grid that tracks what you have, what you use, and what to order. You do not need expensive software to start.
Set up these columns:
- Part number and description
- Grit and size
- Unit of measure
Keep the sheet on a shared drive and update it at every receipt and issue. A common mistake is letting the sheet drift from reality. Count physical stock monthly and reconcile the sheet against it.
Step 2: Run an Abrasive Reorder Point Calculation That Holds Up
An abrasive reorder point calculation sets the stock level that triggers a new order before you run out. The formula is straightforward:
Reorder point = (average weekly usage × lead time in weeks) + safety stock
Say a shop uses 20 belts of one grit per week and the supplier takes two weeks to deliver. If you run custom sizes, you can request a quote for custom sanding belts with your length, width, grit and backing so reorder points match the belts you actually use. Usage during lead time is 40 belts. Add safety stock on top of that.
Where Safety Stock Fits In
Safety stock is the buffer that covers demand spikes and late deliveries. A shop with steady usage can keep it lean. A shop with unpredictable job mix should hold more.
Here is a simple way to set it:
| Usage Pattern | Safety Stock Level | Why |
|---|---|---|
| Steady, predictable | 1 week of usage | Low risk of spikes |
| Seasonal or mixed | 2 weeks of usage | Covers busy stretches |
| Custom or long lead time | 3 weeks of usage | Protects against delays |
Review these levels every quarter. Usage changes with your job mix.
Step 3: Apply Industrial Abrasive Storage Best Practices
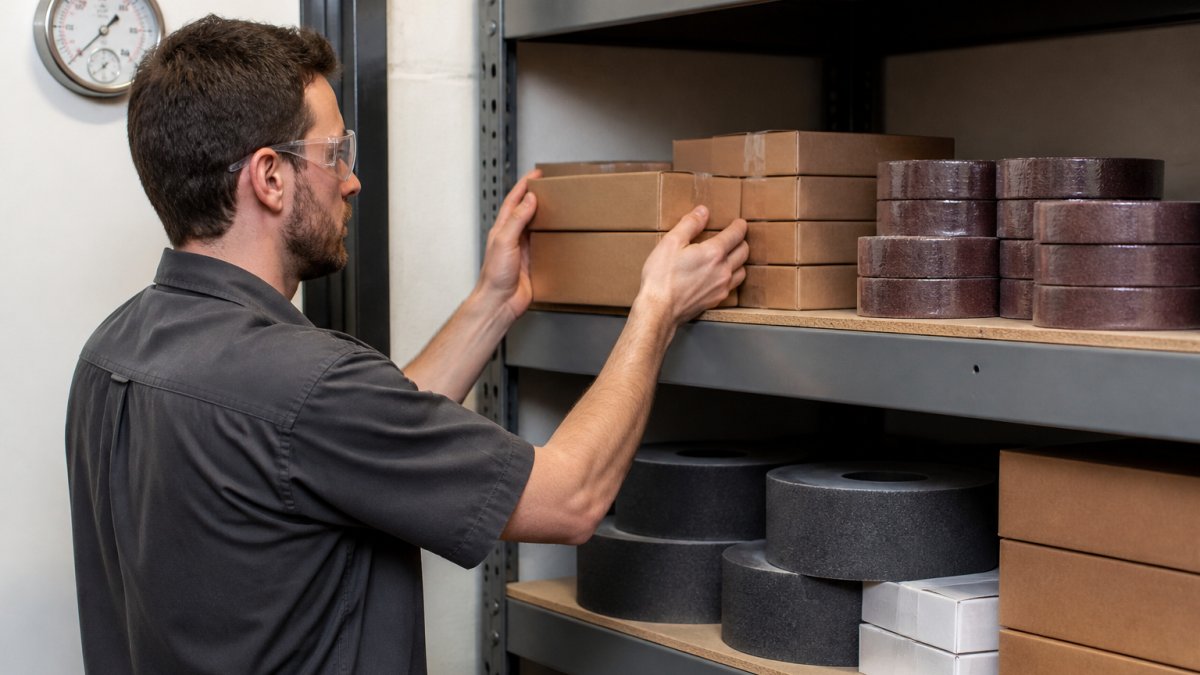
Industrial abrasive storage best practices protect grit sharpness, backing integrity, and shelf life. Coated abrasives are sensitive to moisture and temperature. Store them wrong and you get loading, shedding, and short service life.
Humidity, Temperature, and Original Packaging
Moisture is the enemy. Damp air softens the bond and dulls cutting performance. Keep storage dry and away from loading docks and compressors.
- Keep abrasives in their original packaging until use
- Store flat, not on edge, for belts and sheets
- Keep the area at a stable temperature, away from direct heat
The backing type affects how you store discs, too. If you are unsure whether hook and loop or PSA suits your work, this guide on hook and loop vs PSA sanding discs explains how each holds and how to store them.
Step 4: Choose Abrasive Inventory Tracking Tools That Match Your Shop
Abrasive inventory tracking tools range from a shared spreadsheet to full inventory software. Match the tool to your volume, not to someone else’s setup. The table below shows what each option actually does, where it breaks down, and the rough stockroom size where it starts to pay off.
| Tool | What it does | Where it breaks down | Fits when |
|---|---|---|---|
| Shared spreadsheet | Tracks on-hand, on-order, reorder point, and usage in one grid | Drifts from reality if issues are not logged at the point of use | One person controls stock and SKUs stay under roughly 100 |
| Barcode scanning | Scans receipts and issues so counts update without manual entry | Needs labels on every bin and a scanner at each issue point | Multiple people pull stock and counting errors are frequent |
| Inventory software or ERP module | Ties stock to purchase orders, usage history, and supplier lead times | Overkill if item masters and units of measure are not clean first | Purchasing, receiving, and production all need the same record |
| Supplier dashboards and recurring orders | Lets you reorder fast and set standing shipments for steady items | Does not track internal usage or point-of-use stock | High-volume consumables with predictable draw |
| Vending or kanban at point of use | Puts stock where it is consumed and triggers replenishment on empty | Requires a replenishment owner and a clear min/max per bin | Cells or bays are far from the main stockroom |
Set Up Barcode Labels That Actually Work
A barcode only helps if the label carries the fields your stock sheet needs. Print labels with the part number, grit, size, unit of measure, and lot number. Scan at receipt and at issue, not at month-end.
A common pattern is to start with barcode labels on the top 20 percent of SKUs that drive most usage, then expand once the habit holds.
Use Kanban and Point-of-Use Replenishment for High-Draw Items
Kanban is a simple visual trigger: a bin holds a set quantity, and when it empties, the empty bin itself is the reorder signal. For abrasives, this works well for belts, discs, and blasting media that are pulled every shift.
- Set a min/max for each bin based on one to two weeks of usage.
- Label the bin with the part number, grit, and reorder quantity.
- When the bin hits the min line, the empty container goes to the stockroom or purchasing.
- Refill to max and record the issue on the stock sheet or scanner.
Point-of-use replenishment keeps stock close to the sander or blast cabinet without letting it pile up out of sight. The trade-off is that you need a named person to check bins on a set schedule, or the kanban cards go unnoticed.
Fix your stock records before you buy software. A clean spreadsheet with accurate counts beats an ERP that nobody trusts.
When you are ready to see the actual brands and grit ranges you would be tracking, browse the Sia abrasives in stock to build your item list from real part numbers.
Step 5: Rotate Stock with FIFO and Lot Traceability
FIFO means first in, first out: the oldest stock gets used first. Lot traceability means you can trace a box back to its batch. Together they protect quality and stop dead stock from piling up.
Put these habits in place:
- Load new stock behind old stock on the shelf
- Label each box with the receipt date
- Record the lot number on the stock sheet
If a batch performs poorly, lot records let you pull it fast and tell your supplier. That is quality control you cannot get from guesswork.
Step 6: Standardize SKUs and Track the KPIs That Matter
SKU rationalization means cutting duplicate and near-duplicate items so your stock stays simple. Fewer SKUs mean fewer stockouts, less dead stock, and faster counting. Start by grouping abrasives by grit and format, then look for overlaps: two suppliers’ 120-grit belts in the same size, three disc backing types where one covers the work, or a grit ladder with gaps and near-duplicates.
A practical way to rationalize:
- List every abrasive SKU with its grit, size, backing, and annual usage.
- Flag SKUs with low usage that duplicate another item’s function.
- Keep the item with the better lead time, price, or performance record.
- Retire the rest and update the stock sheet and bin labels.
- Standardize new purchases against the surviving list.
The KPIs and How to Calculate Them
Track a handful of inventory KPIs with real formulas so the numbers mean something:
- Inventory turnover: cost of abrasives consumed divided by average inventory value over the same period. A higher number means stock moves faster; a very low number points to dead or slow stock.
- Stockout rate: number of stockout events divided by total issue requests. Count a stockout whenever an item hits zero when someone needs it.
- Carrying cost: the cost of holding stock, including storage space, handling, insurance, and capital tied up. Many shops estimate this as a percentage of average inventory value rather than tracking every line.
A Worked Example
Suppose a shop consumed $48,000 CAD of abrasives last year and carried an average inventory value of $12,000 CAD. Inventory turnover is 48,000 divided by 12,000, or 4 turns per year. If the same shop logged 30 stockout events against 600 issue requests, the stockout rate is 5 percent. Those two numbers alone tell you whether to focus on excess stock or on replenishment timing.
Pick two or three KPIs, calculate them the same way every month, and act on the trend. A simple turnover and stockout rate reviewed monthly beats a dashboard nobody reads.
To build clean, standardized SKUs, you need real part numbers and grit ladders. The Sia 1950 Siaspeed series shows disc, sheet, and roll formats from 40 to 1500 grit so you can standardize against actual specs.
Common Mistakes That Undermine Abrasive Stock Control
The biggest mistakes are simple and repeatable. Fix these and most stock problems disappear.
- Ordering discs with the wrong hole pattern, creating dead stock. Check a sanding disc hole pattern fit chart before you buy.
- Letting the stock sheet drift from physical counts
- Storing abrasives in damp areas near doors or compressors
Watch out: storing coated abrasives in a humid corner can ruin a whole batch before it ever touches a sander. The loss shows up as poor cutting performance and early wear, not as an obvious defect.
Frequently Asked Questions
How should industrial abrasives be stored?
Keep coated abrasives and grinding wheels in their original packaging, on dry shelving away from floor moisture, and in a space where humidity stays stable. Belts and discs can curl or lose grain adhesion when exposed to damp air, so avoid unheated corners and leaky roofs. Stack boxes flat rather than on edge, keep them off concrete, and rotate older lots to the front. A simple humidity gauge on the wall tells you when conditions are drifting.
How do you track abrasive inventory in a manufacturing shop?
Start with a stock control spreadsheet that logs SKU, grit size, quantity on hand, reorder point, lead time, and lot number. Count high-use items weekly and the rest monthly. When volume grows past a few hundred SKUs, move to barcode scanning or a lightweight inventory app tied to your purchase orders. The key is one record everyone trusts, updated at point of use rather than at month end.
How much abrasive inventory should a shop keep on hand?
Enough to cover your average usage during supplier lead time plus a safety buffer for demand spikes. Calculate it: daily usage multiplied by lead time in days, plus safety stock. A metal fab shop burning 40 discs a day with a 10-day lead time needs at least 400 discs before the buffer. Keep the buffer lean for slow movers and generous for anything that stops the line when it runs out.
When should abrasive products be reordered?
Reorder when stock hits the reorder point, not when the shelf looks empty. Set that point as daily usage times lead time plus safety stock, then review it quarterly as usage shifts. For critical grits and belts, consider automated recurring shipments so replenishment happens on a schedule rather than after a scramble. A supplier that supports purchase orders and scheduled deliveries removes most of the guesswork.
Managing industrial abrasive inventory comes down to clean records, honest reorder points, and dry storage. When the admin work piles up, that is where IBEX Enterprises helps. Our platform supports purchase order payments, automated recurring shipments, and rapid reordering from a personalized dashboard, so your shop stays stocked without the weekly scramble. Get started with IBEX Enterprises and keep your line running.