Last Updated: November 19, 2026
Quick Summary
The best practices for shop inventory management are to keep one centralized record for every SKU, set reorder points using the formula (average daily usage × lead time) + safety stock, and count stock on a rotating cycle instead of one annual shutdown. Track cheap consumables like abrasives as tightly as tools, because a missing disc stops a job.
- Assign every item a fixed stock location and label the bin, not just the item.
- ABC analysis sorts stock into three tiers so you watch your top ten items closely.
- Cycle count A-items weekly, B-items monthly, and C-items quarterly.
- Match the software to shop size and price total cost of ownership over three years.
- Trace each count discrepancy to unlogged use, receiving error, damage, or untracked returns.
Table of Contents
- Why Shop Inventory Management Decides Whether Your Jobs Ship On Time
- Building a Centralized Inventory Record for Every SKU
- The Inventory Reorder Point Formula That Prevents Stockouts
- How ABC Inventory Analysis Focuses Your Attention on What Matters
- Cycle Counting Inventory Instead of Shutting Down for a Full Count
- Choosing Inventory Management Software for Small Business Shops
- Demand Forecasting From Sales History and Seasonality
- Cutting Shrinkage, Theft, Damage, and Returns
- Frequently Asked Questions
Why Shop Inventory Management Decides Whether Your Jobs Ship On Time
Shop inventory management is the practice of tracking, controlling, and replenishing every consumable and tool in a working shop so jobs finish on schedule. In woodworking, fabrication, and body shops, late jobs rarely fail because of labor or equipment.
Abrasives disappear faster than most owners expect. Sanding discs get used up, belts wear out, and nobody logs it. Then a Friday afternoon job grinds to a halt over a missing grit.
Building a Centralized Inventory Record for Every SKU
Every SKU in your shop needs one record, in one place, with one owner: a single list of every stocked item with its quantity, location, reorder threshold, and supplier.
Build the record with these fields for every item:
- SKU code and description
- Unit of measure, such as discs per box or rolls per case
- Current quantity on hand
A common mistake is tracking only high-value items. Consumables like sandpaper and grinding discs are cheap individually but stop a job dead when they run out. Track them with the same discipline as your tools.
Stock Locations and Barcode Tracking That Hold Up on the Floor
A record only works if the physical shelf matches it. Assign every item a fixed stock location and label the bin, not just the item. Barcode scanning at the point of use closes the loop: a worker scans a box out, and the count updates in real time. Barcode labels fail in dusty shops, though, so use laminated or metal-backed labels and reprint any that peel, or your inventory accuracy quietly erodes.
The Inventory Reorder Point Formula That Prevents Stockouts
The inventory reorder point formula is: reorder point = (average daily usage × lead time in days) + safety stock. A shop using 20 discs a day with a 10-day lead time and 50 discs of safety stock reorders at 250 discs.
Most shops reorder when the shelf looks low. That is too late. Lead times stretch, shipments get delayed, and the stockout hits during your busiest week. Calculating reorder points for your top consumables removes the guesswork.
A purchase order system pairs naturally with reorder points: when a count crosses the threshold, a PO goes out immediately rather than waiting for someone to notice. You can see how purchase orders keep your supply room stocked alongside a working reorder system. To remove the manual step entirely, automating abrasive reordering connects the threshold to a standing order.
Setting Par Levels and Safety Stock for Abrasives and Consumables
Par level is the maximum you keep on hand; safety stock is the buffer above expected usage. Because abrasives come in so many grits, choosing the right sanding grit first tells you which ones you actually burn through. And since grit and backing degrade with moisture and heat, how industrial abrasives should be stored matters as much as how many you keep: a full shelf of ruined discs is still a stockout.
How ABC Inventory Analysis Focuses Your Attention on What Matters
ABC inventory analysis sorts your stock into three tiers by value and usage, so you spend management time where it pays. A-items are high-value, high-turnover products that deserve tight control and frequent review. B-items need routine attention. C-items are low-cost, high-volume consumables that can run on simple rules.
For most shops, the A-list is short: your most-used grits, your core grinding discs, and any item with a long lead time. Give those a weekly count and a firm reorder point. C-items can sit on automatic replenishment.
Cycle Counting Inventory Instead of Shutting Down for a Full Count
Cycle counting inventory means counting a small slice of your stock on a rotating schedule instead of closing the shop for one annual physical count.
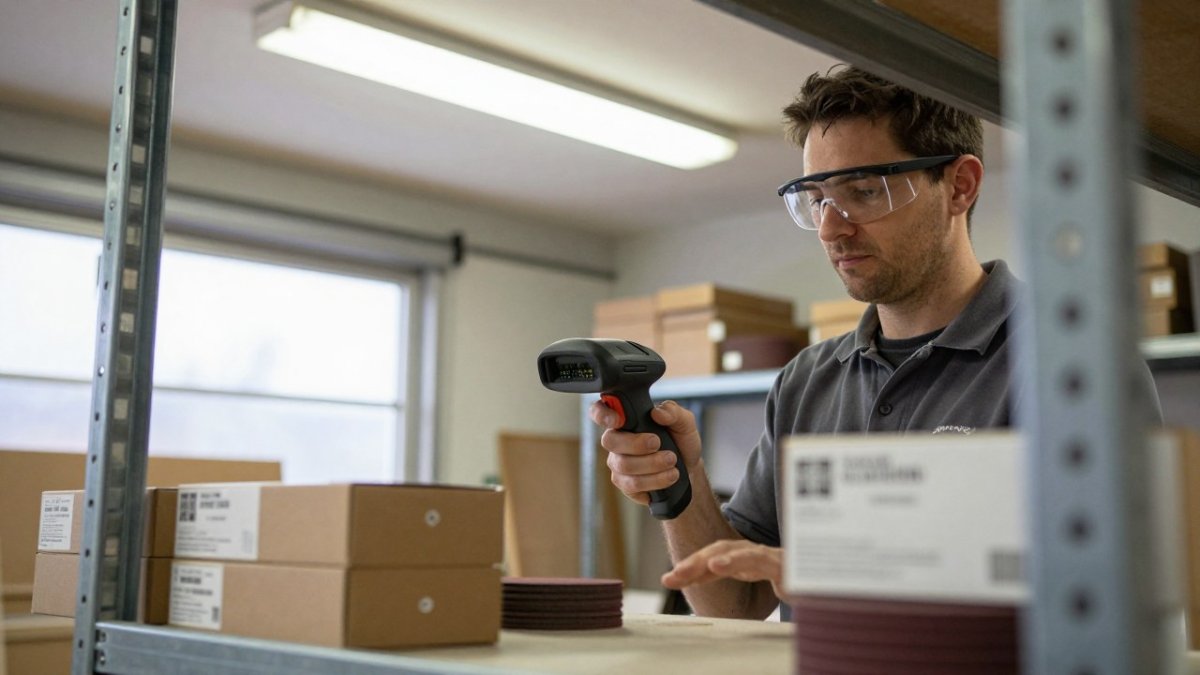
Start with your A-items and count them weekly. Add B-items monthly and C-items quarterly.
Choosing Inventory Management Software for Small Business Shops
Inventory management software for small business should solve three problems: accurate stock tracking, automatic reorder alerts, and clean purchase records. Everything else is optional. A shop does not need a full enterprise platform; it needs a system the team will actually use every day. The trap is buying on feature count instead of total cost of ownership, then discovering the real expense is hours spent reconciling integrations and retraining staff.
A Neutral Selection Checklist by Shop Size
Match the tool to the operation, not the other way around. A one-bay fabrication shop with two staff and a single point-of-sale terminal has different needs than a multi-location body shop with a backroom, a front counter, and an online parts store.
- Single-location, under five users: barcode scanning, reorder-point alerts, purchase order creation, and a mobile view for the floor. A spreadsheet can survive here only if someone owns it daily.
- Single-location, five to twenty users: role-based permissions, stock by location and bin, receiving against a PO, and reporting on usage by SKU and by job.
- Multi-location or omnichannel: real-time synchronization across the shop, online store, marketplaces, and point-of-sale; reservation and return handling; and an audit trail so a count discrepancy can be traced to a transaction.
Integrations and Barcode Support That Decide the Real Cost
Ask what the system connects to before you ask what it costs.
Barcode support deserves its own test. Confirm the system accepts the symbologies your suppliers already print, works with a handheld scanner rated for dust and drops, and lets you print laminated or metal-backed shelf labels from inside the tool.
Watch out: a demo that runs on clean sample data will not show you how the system handles a partial receipt, a backorder, or a return-to-stock, ask to run those three transactions live before you sign.
Total Cost of Ownership Beyond the Subscription
Price the whole system over three years, not the monthly seat fee. The line items that surprise shops are per-user or per-location add-ons, scanner and label-printer hardware, onboarding and data migration, integration or API fees, payment processing on purchase orders, and staff hours to clean up the item master before go-live. A lower subscription with a paid integration can cost more than a higher subscription that connects natively to your accounting and point-of-sale.
A 30/60/90-Day Rollout and Staff Accountability Plan
Software fails when it is switched on without a plan. Phase it.
- Days 1-30: clean the item master, assign one owner per stock area, label bins, and run the new system in parallel with the old method on your top A-items only.
- Days 31-60: move all receiving and scan-out to the new system, retire the parallel record, and train each role on the three transactions they perform most (receive, issue, reorder).
- Days 61-90: turn on reorder alerts and reporting, review the first month of usage data, and set a weekly cycle-count schedule tied to the system’s discrepancy report.
Assign accountability by role, not by hope: a receiving owner, a replenishment owner, and a count owner. Write the three responsibilities into the job description so the system has a human backstop. IBEX Enterprises offers a B2B platform with recurring shipment subscriptions, purchase order payment options, and rapid reordering from a personalized dashboard, which can help keep the ordering step from becoming a separate project.
Demand Forecasting From Sales History and Seasonality
Demand forecasting uses your own sales history to predict what you will need next. Pull the last twelve months of usage per SKU and look for patterns: which grits spike before busy season, which jobs consume the most discs, and where usage swings month to month.
Seasonality matters in a shop as much as in retail. Demand in these trades often ramps with seasonal and project cycles. Forecast against those curves rather than a flat average.
Cutting Shrinkage, Theft, Damage, and Returns
Shrinkage is the gap between what your records say you have and what is actually on the shelf. In a shop, most of it is not theft. It is unlogged use, damaged stock, and returns that never make it back into the count. Each one is fixable, but only if you can tell them apart. The unique angle most guides skip is the investigation: how to trace a discrepancy to its source instead of writing it off.
Measure Shrinkage Before You Attack It
Start with a shrinkage rate so you have a baseline. Count a defined set of SKUs, compare the physical count to the record, and express the gap as a percentage of the recorded quantity or value for that set. Do this on the same SKUs every period so the number is comparable. A rising rate on one category points to a process problem; a flat rate spread evenly usually points to unlogged use.
Trace Every Discrepancy to One of Four Causes
When a cycle count does not match, do not adjust the number and move on. Work backward through the transaction trail and assign the miss to one of four causes:
- Unlogged use: the item left the shelf without a scan. Look for a pattern by shift, by job, or by worker. The fix is making scan-out the only path to the shelf, not a reminder.
- Receiving error: the PO said ten cases, the dock got eight. Check the receiving record against the supplier’s packing slip before the stock hits the shelf.
- Damage or spoilage: abrasives degrade with moisture and heat, and damaged stock is still a shortage. First-in-first-out rotation and controlled storage prevent most of it.
Watch out: a recurring miss on a single SKU is almost never random, it usually traces to one receiving error or one unlogged grab point, so investigate the pattern before you change the reorder point.
Controls That Actually Reduce Loss
Put the strongest controls where the loss is largest. Barcode scan-out at the point of use is the single highest-impact control because unlogged use is usually the biggest bucket.
| Problem | Control | How to verify it worked |
|---|---|---|
| Unlogged use | Barcode scan-out at point of use | Shrinkage rate on that SKU falls next count |
| Receiving error | Match packing slip to PO before shelving | Fewer receiving discrepancies on the PO log |
| Damaged abrasives | Controlled storage, FIFO rotation | Lower write-off quantity per period |
| Untracked returns | Defined return-to-stock step | Returns appear in the count, not as shortages |
| Theft | Locked storage for high-value items | Shrinkage rate on locked SKUs stays flat |
Run a cycle count on your highest-shrinkage SKUs first and you will find the leak quickly.
Running a shop means juggling jobs, staff, and deadlines. Inventory should not be another fire to fight.
Frequently Asked Questions
What are the best practices for shop inventory management?
Start with one centralized inventory record for every SKU, including abrasives, tools, and protective gear. Assign each item a stock location and track it with barcode scanning or a point of sale system. Set reorder points and par levels based on lead time and average usage, then run cycle counts on a rolling schedule instead of one annual physical count. Rank products with ABC inventory analysis so your highest-value and highest-turnover items get checked most often. Review inventory turnover and carrying costs monthly, and automate replenishment wherever usage is predictable.
How do you set reorder points for shop supplies?
Use the inventory reorder point formula: reorder point equals average daily usage multiplied by lead time in days, plus safety stock. If your shop uses 20 sanding discs a day and your supplier takes five days to deliver, that is 100 discs of lead-time demand. Add safety stock, say 30 discs for demand spikes, and you reorder at 130. Review the numbers quarterly, because usage shifts with job mix and seasonality. For critical items, build in extra buffer or set up automated recurring shipments so replenishment does not depend on someone remembering to check.
How often should a shop count its inventory?
Most shops do better with cycle counting than a single annual physical inventory count. Count high-value A items monthly, B items quarterly, and C items once or twice a year. That spreads the work across the calendar, keeps inventory accuracy high, and avoids shutting down operations for a full count. If your records drift more than a few percent, increase the frequency on the problem categories. Many shops count a small number of SKUs every day so the whole catalog is verified on a rolling basis.
What is the difference between inventory management and inventory control?
Inventory management is the broader strategy: demand forecasting, purchasing decisions, supplier management, storage layout, and how much cash you tie up in stock. Inventory control is the day-to-day execution: tracking stock levels, recording receipts and issues, cycle counting, and keeping the inventory records accurate. A shop needs both. Control keeps the numbers true, while management decides what those numbers should be. Weak control undermines even a good management plan, because forecasts built on inaccurate records produce the wrong reorder points.
How can a shop prevent stockouts without overordering?
Tie ordering to data rather than habit. Calculate reorder points from actual usage and lead time, keep safety stock sized to real demand variability, and use ABC inventory analysis to give critical items tighter review. Track stockout and overstock incidents so you can see which SKUs keep causing problems. For consumables with steady usage, automated recurring shipments remove the guesswork. For unpredictable items, order smaller quantities more often. Review excess inventory quarterly and cut order quantities on slow movers before carrying costs eat the savings.
Which inventory metrics should purchasing teams track?
Track inventory turnover (cost of goods sold divided by average inventory value), days of inventory on hand, stockout rate, inventory accuracy from cycle counts, and carrying costs as a share of inventory value. Add fill rate or customer service level so you know how often you could fill a request from stock. Review these monthly against your own baseline rather than industry averages. A shop with accurate records and a rising turnover ratio is usually freeing up cash flow without hurting availability.